$1,079.16
$1,046.78
Tax included
World's First Climate Tech Platform | Free Delivery in India | Global Shipping

Shop with confidence knowing that our 24/7 Customer Support is always available to assist with any inquiries

Avail maximum benefits from input tax mechanism on all your Business Invoices. Get GST Invoices on your business purchases. And 0% Taxes on all worldwide deliveries

If you find this product anywhere at lower cost than us. Call us and we will not only match the price but also give a complimentary coupon

Shop with assurance, as each product we offer is 100% original, ensuring quality and authenticity with every purchase
| Country of Origin | Germany |
|---|---|
| Diameter | 500mm |
| Brand | ProMinent |
| Material | Polyethylene |
| Height | 760mm |
| Model | 1001490 |
| Volume | 100L |
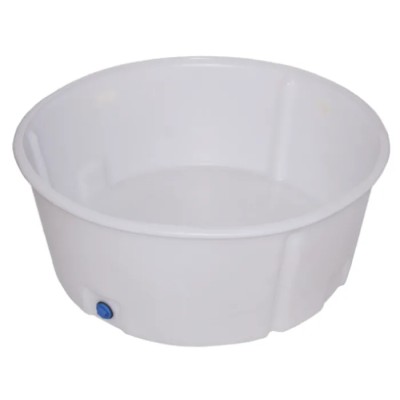
ProMinent 1001490 Polyethylene Chemical Tank is purpose-built for safe storage and accurate dosing of chemicals in industrial facilities. With a robust design and high-quality materials, this 100 litre tank is suitable for chemical, pharmaceutical and beverage applications requiring reliable fluid handling.
Manufactured from UV-stabilised polyethylene, ensuring long-term resistance to chemical exposure and sunlight. The tank's flat sides simplify securing and mounting operations within plant environments. Integrated scales in both litres and gallons deliver easy and accurate monitoring of tank contents.
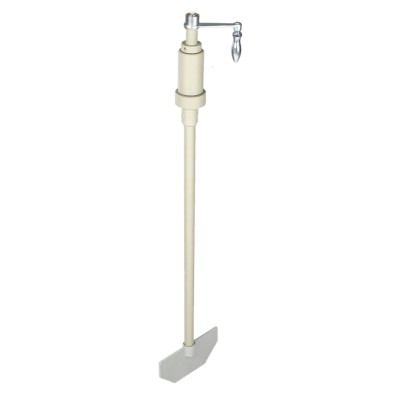
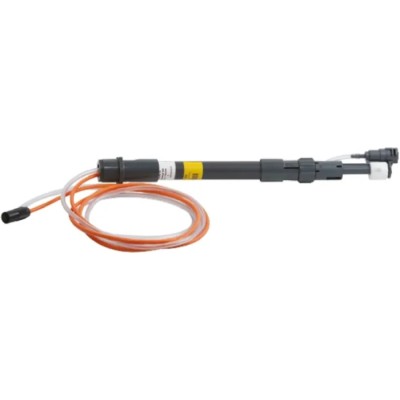
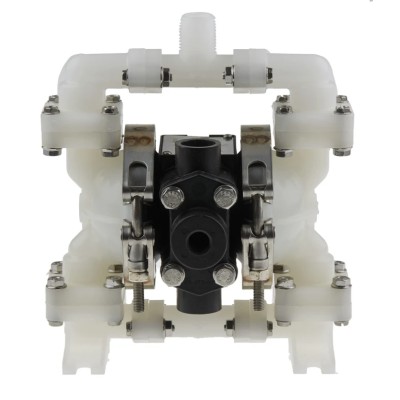
Sintered threaded sockets allow direct fitting of ProMinent metering pumps, suction lances or stirrers, streamlining installation and system integration. The screw-on lid provides safe enclosure, minimising risk of spills or contamination when not in use.
Designed to meet the needs of chemical dosing, storage and transfer in demanding scenarios such as water treatment, pharmaceutical production, and food and beverage operations. Black in colour with sturdy construction to withstand harsh environments.
This tank is engineered to comply with operational standards relevant to industrial chemical storage, although formal certifications are not specified for this model. Its compatibility with ProMinent metering pump ranges enhances process efficiency and safety.
Use cases include plant chemical storage, dosing systems for industrial water treatment, laboratory fluid management, and process control in manufacturing. Explore the ProMinent category and Chemical Storage Tanks for more advanced solutions and industrial-grade tanks on EnvMart.
Review sent
Your review cannot be sent
Global Payments 140+ Countries
Global Shipping Fedex/UPS/DHL/Aramex/
BlueDart/Delhivery/DP World
24/7 Customer Support Email/Chat/Telephonic Support
Comments (0)
Your review appreciation cannot be sent
Report comment
Report sent
Your report cannot be sent